A part that has run without complaint for years suddenly starts cracking, warping or failing an incoming inspection. The drawing has not changed. The mold has not changed. The process sheet has not changed. When the investigation finally reaches the resin, the answer is often uncomfortable: the material arriving on the dock is no longer quite the material that was qualified, and nobody in the chain thought the change was worth mentioning.
Material variation from suppliers is not new, but the conditions that drive it have intensified. Resin producers consolidate plants and rationalize grade portfolios. Compounders switch additive packages when a stabilizer or pigment becomes scarce or restricted. Distributors substitute "equivalent" grades to fill an order. Recycled content is being blended into products that were qualified on virgin material. Each change may be defensible on its own terms. Collectively, they mean that a qualification performed once, years ago, is a weaker guarantee than most purchasing and quality teams assume.
What "equivalent" usually means
The word that causes the most trouble in materials supply is "equivalent". To a supplier it typically means that the replacement grade meets the same headline datasheet values: similar melt flow, similar tensile strength, similar heat deflection temperature. To the part, equivalence means something narrower and harder to prove: the same behavior in this geometry, under this load, in this environment, for this service life.
Datasheet values are measured on standardized specimens under standardized conditions. They say little about long-term creep, fatigue, chemical resistance, weld-line strength, low-temperature toughness or how a material responds to the specific molding conditions in your plant. Two grades with near-identical datasheets can diverge sharply on exactly the property that keeps your part alive.
Where the changes hide
Material changes rarely announce themselves. The most common routes are:
- Additive package changes. Stabilizers, lubricants, nucleating agents and impact modifiers are reformulated for cost, regulatory or supply reasons. These changes can alter UV durability, thermal aging, mold release behavior and toughness without moving the headline datasheet numbers much.
- Plant or line transfers. The same grade name produced at a different site can differ in molecular weight distribution, residual catalyst or gel content.
- Distributor substitution. Under supply pressure, a "drop-in" grade from another producer is shipped under a purchase order written for the original.
- Colorant and masterbatch changes. Pigments interact with polymers. Some nucleate crystallization and change shrinkage and warpage; others affect weathering.
- Recycled or regrind content. Introduced for cost or sustainability targets, often without a full requalification of the parts affected.
Why the pressure is rising now
Two forces are making material changes more frequent. The first is regulatory. Restrictions on certain flame retardants, plasticizers, per- and polyfluoroalkyl substances used as processing aids, and other additives are prompting compounders to reformulate established grades. A reformulation driven by compliance is entirely legitimate, but a replacement additive rarely behaves identically to the one it replaces, and the downstream user is often the last to find out. The second is sustainability. Customer and regulatory targets for recycled content are pushing post-consumer and post-industrial material into products qualified on virgin resin. Recycled feedstocks bring variability in molecular weight, residual contamination and additive history that a virgin grade does not have.
Neither trend is going away. Both mean that the material in a given part number is more likely to change during the life of a program than it was a decade ago, and that the qualification evidence on file is more likely to describe a material that no longer ships.
What to ask when a supplier announces a change
A notification is only useful if it prompts the right questions. When a supplier announces a change, ask for:
- The nature of the change in specific terms: which ingredient, which site, which process step.
- The supplier's own comparison data, including properties beyond the datasheet, and the test conditions used.
- Retained samples of both old and new material so that you can run your own fingerprint and part-level tests.
- The last-time-buy option on the current material, which buys time to requalify without schedule pressure.
- The regulatory driver, if any, so you can judge whether other suppliers will face the same change.
Suppliers that answer these questions clearly are usually managing change well. Suppliers that cannot are telling you something important about the risk you carry.
Building a change-control net that actually catches changes
Three layers of control work together. None is sufficient alone.
Contractual: make notification an obligation
A purchase specification should require advance written notice of any change to formulation, manufacturing site, raw material source or process that could affect performance, with enough lead time to evaluate it. It should name the exact grade and supplier, prohibit substitution without written approval, and give you the right to receive certificates of analysis for each lot. These clauses are common in automotive and medical supply chains; they are far less common, and far less enforced, elsewhere.
Technical: fingerprint what arrives
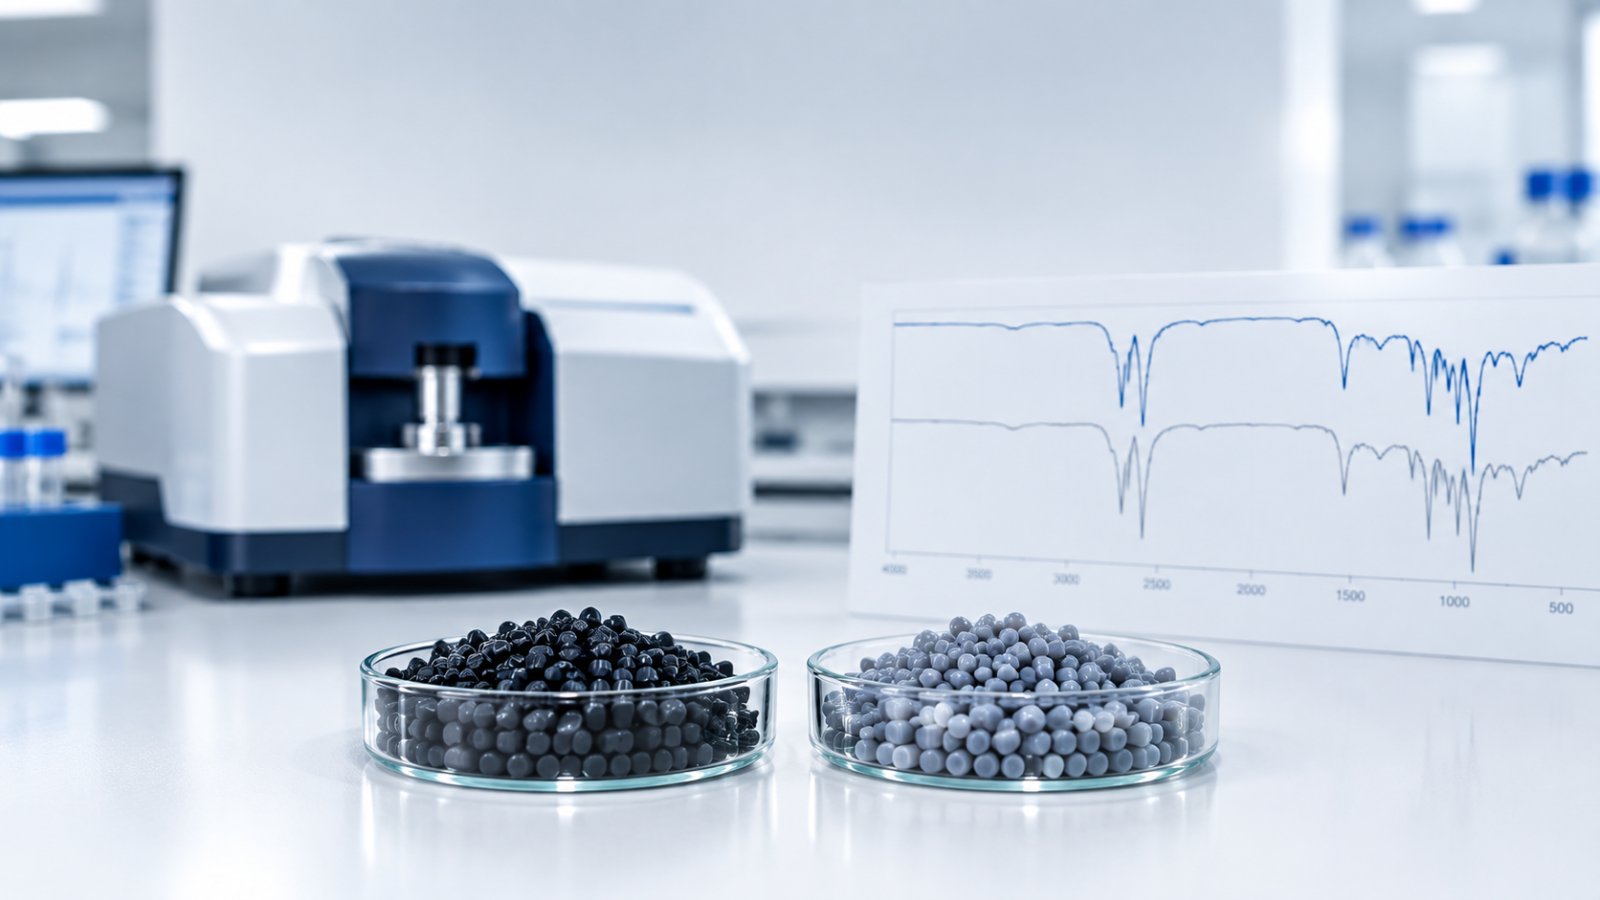
Contracts only work if you can detect a breach. A material fingerprint is a small set of quick, inexpensive tests that characterize the qualified material, run periodically on incoming lots and compared against a baseline. A practical fingerprint for most thermoplastics includes:
- FTIR spectroscopy to confirm polymer identity and flag additive or contamination changes.
- DSC to compare melting, crystallization and glass transition behavior, which shift with nucleation, blending and grade changes.
- Melt flow rate to track molecular weight consistency.
- TGA or ash content to confirm filler and reinforcement levels in filled grades.
The point is not to re-qualify every lot. It is to notice, early and cheaply, when a lot stops looking like the material you approved. A retained sample of the original qualified lot, properly stored, makes every later comparison far more powerful.
Engineering: requalify in proportion to risk
When a change is detected or announced, the response should be proportionate. A colorant change on a decorative cover does not need the same evaluation as a stabilizer change on a pressurized fitting. A sensible requalification plan starts by asking which properties the part's function and failure modes actually depend on, then tests those on molded parts, not just plaques: weld-line strength if the part has weld lines, chemical resistance if it sees fluids, long-term aging if it lives outdoors or hot.
Fingerprinting has limits worth acknowledging. It is good at detecting that something changed and poor at predicting whether the change matters. A small shift in a DSC trace might be harmless, or it might signal a nucleation change that will alter warpage on a thin-walled part. That is why a detected change should trigger engineering judgment, not an automatic rejection, and why the requalification plan matters as much as the test.
The cost of getting this wrong
When an unannounced change causes a field failure, the commercial consequences arrive in a predictable order: containment and sorting, line disruption, warranty costs, and then the question of who pays. That last question turns on documents. Did the specification require notification? Did the supplier certify conformance? Did the buyer have a way to detect the change and fail to use it? Companies with a clear specification, a retained baseline sample and a fingerprinting record are in a strong position to recover costs. Companies relying on a grade name and a handshake usually are not.
The same records are central if a failure reaches litigation. An independent comparison of the failed part, the retained baseline and the supplier's lot data is often the most persuasive evidence available on whether a change occurred and whether it caused the failure.
Practical steps for this quarter
- Audit your critical parts. List the components whose failure would be expensive, and confirm each has a named grade, a no-substitution clause and a notification requirement.
- Establish baselines. Retain and fingerprint samples of the currently approved material for each critical grade.
- Set a sampling rhythm. Fingerprint incoming lots at a frequency that reflects risk and supplier history.
- Write the requalification playbook in advance. Decide now which tests each part family needs when a change occurs, so the decision is not made under schedule pressure.
Material variation is a supply chain reality. Being surprised by it is optional.
If you are evaluating a supplier change, chasing an unexplained shift in part performance, or building a qualification and fingerprinting program, Flaney Associates provides independent materials selection and qualification support. Discuss Your Challenge at flaneyassociates.com/contact.html or Get the Checklist at flaneyassociates.com/checklist.html.
Written by Joshua U. Otaigbe, PhD